HOT-DIP GALVANIZING PROCESS
A tried and tested process.
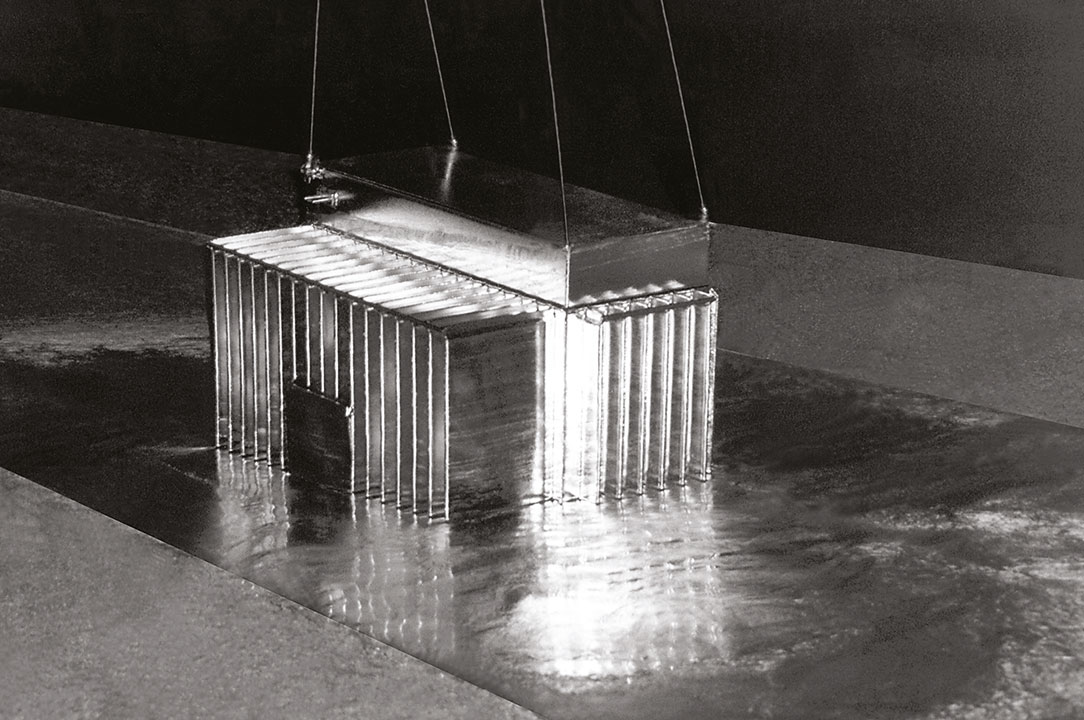
Hot-dip galvanizing applies a zinc coating to steel or cast-iron components by immersing them in a bath of molten zinc.
The simplicity of the process is an advantage over other methods of corrosion protection.
Our process has eight stages:
1. Degreasing – Bath in an acid solution to remove oils, greases and other contaminants.
2. Rinsing – Water rinse to prevent contamination of the following baths.
3. Pickling – Bath in commercial hydrochloric acid to remove oxides and mill scale.
4. Rinsing – A second rinse to prevent contamination of the following baths.
5. Fluxing – A zinc chloride and ammonium chloride solution that protects the part from oxidation between pickling and immersion in zinc. It also acts as a wetting agent in the zinc bath.
6. Drying – Drying in an oven at 60 °C to dry the parts and reduce thermal shock on immersion in the zinc bath.
7. Zinc bath – Immersion in molten zinc at 440 °C to 465 °C. The iron–zinc (Fe/Zn) reaction forms the final coating.
8. Passivation – Passivation increases the part’s resistance and, therefore, its durability.